
 Insert molding
 Overmolding
 Unscrewing molds
 Automotive
 Electronics
 Home appliance
 Industrial equipment
 Medical devices
 Machinery & automation


Automotive
Bump Exterior Automotive Part
30% GF PA66 exterior bumper grille insert from a two-cavity H13 HASCO mold.
30% GF filled PA66AISI H132 cavities
Engineering details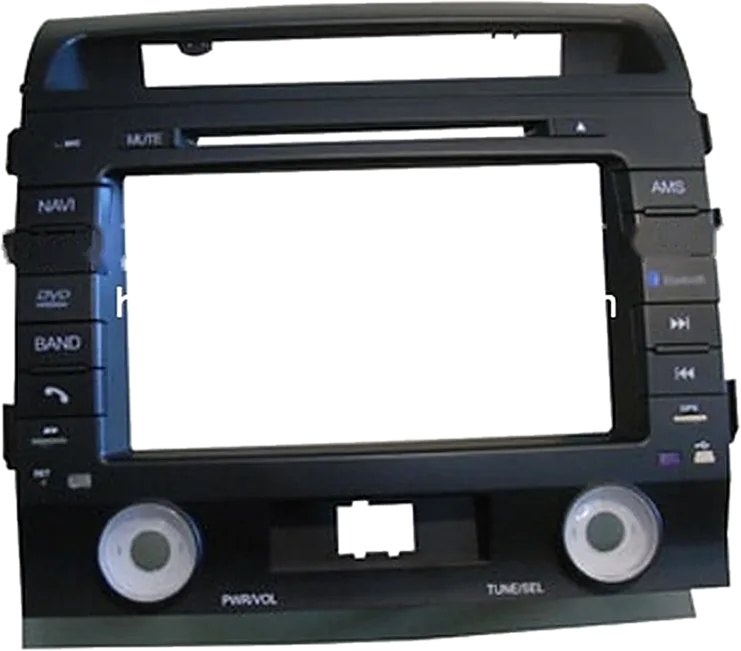 Click to zoom
Low-volume tooling for aftermarket dash and panel parts in 30% GF PA66, built to HASCO or DME.
| Part material | 30% GF filled PA66 |
|---|---|
| Cavity / core steel | AISI H13 |
| Runner system | Cold runner |
| Cavities | 2 cavities |
| Processing | Plastic molding |
| Mold standard | HASCO |
Aftermarket panels such as this navigation bezel are sold in hundreds or a few thousand units, not millions. Sometimes the total value of the parts is lower than the cost of the mold, so the tooling has to be sized to the real volume. We build short-run molds for panel parts in 30% glass-filled PA66, to HASCO or DME standards, with hot or cold runners.
Mold life for these programs typically runs from 1,000 to 100,000 shots. For simple panel shapes we can cut the cavity and core directly into P20 A and B plates instead of using separate inserts. That saves steel, machining time and money, and because the cavity is one solid block it is often stronger than an inserted design. With adequate maintenance such a mold can reach 300,000 shots.
High-volume molders are set up for long runs; changeovers and small batches cost them money. We run 14 presses of different sizes and our own tool shop, so a short run is a normal job for us rather than an interruption.
| Part material | 30% GF filled PA66 |
|---|---|
| Tooling made in | China |
| Cavity / core steel | AISI H13 |
| Runner system | Cold runner |
| Cavities | 2 cavities |
| Customer | Auto injection molding company |
| Processing | Plastic molding |
| Mold standard | HASCO |
| Category | Automotive Parts |
Typical applications for this kind of part:
Send the drawing and we will quote it using this project as a reference.
Our after-sales team supports mold maintenance and modifications remotely and can supply spare inserts. Contact customerservice@precisemoulds.com.
Usually from about 100 to 10,000 parts per year. At these volumes the tooling cost per part matters more than cycle time, so mold design focuses on simple, low-cost construction.
Short-run molds can have simpler cooling, so we compensate with gate location studies, uniform wall thickness, rib-to-wall ratios of 40–60% and controlled packing in the process. Moldflow is used when the geometry is critical.
Yes. A P20 short-run mold can be replaced by, or supplemented with, a hardened multi-cavity production mold. Keeping the same part design means the change is mostly tooling.
More automotive parts engineered by our team.
30% GF PA66 exterior bumper grille insert from a two-cavity H13 HASCO mold.
Large 15% GF PA66 interior panel from a single-cavity DIN 1.2311 hot-runner mold with multiple inserts.
Pair of 30% GF PA66 interior components molded in a two-cavity H13 HASCO mold.
Left- and right-hand exterior trim pair in 30% GF PA66, two-cavity H13 HASCO mold.
Get a quote
Share a 3D file, 2D drawing, sample photo or sketch. A mold engineer — not a sales robot — checks moldability before we quote tooling and part price.


