
 Insert molding
 Overmolding
 Unscrewing molds
 Automotive
 Electronics
 Home appliance
 Industrial equipment
 Medical devices
 Machinery & automation


MoldHot runner
Automotive
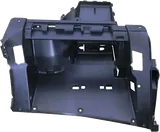
Mold Making for Automotive Cabinet Parts
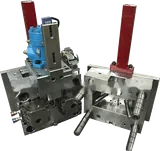
Single-cavity DIN 1.2344 mold with a YUDO hot runner, lifters and slides for a 20% GF PA66 interior cabinet.
20% GF filled PA66DIN 1.2344Single cavity
Engineering details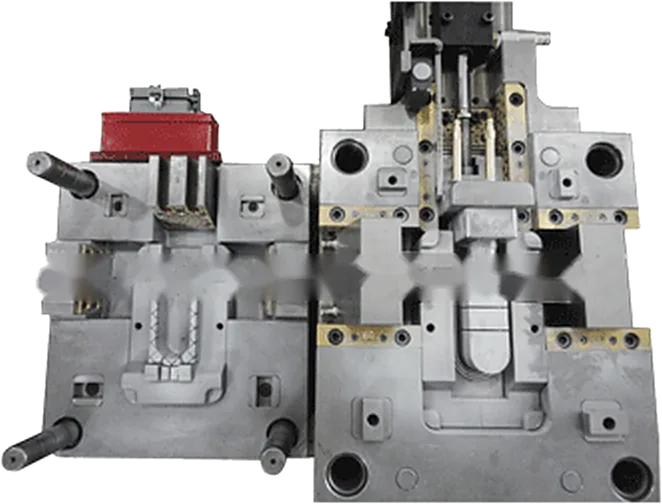 Click to zoom
Hot-runner H13 production mold for 30% GF PA66 precision parts, built for long life.
| Part material | 30% GF filled PA66 |
|---|---|
| Cavity / core steel | AISI H13 |
| Runner system | Hot runner |
| Cavities | Single cavity |
| Processing | Plastic molding |
| Mold standard | HASCO |
Mold making for high-volume injection molding is a different discipline from low-volume tooling. When a mold must run for years and produce millions of parts, every component needs tight tolerances so each part is consistent and fits with others. Automotive parts, consumer electronics and medical devices all depend on molds that withstand high pressure and keep their shape under stress.
A high-volume mold costs more at the start, but it lowers the cost of every part. Saving one second of cycle time or one gram of runner per shot adds up to a large sum over a million parts. We present these trade-offs in the quotation so you can choose the right level of investment.
All critical components are measured on CMM, and the mold is delivered with drawings, a spare parts list and a maintenance plan.
| Part material | 30% GF filled PA66 |
|---|---|
| Tooling made in | China |
| Cavity / core steel | AISI H13 |
| Runner system | Hot runner |
| Cavities | Single cavity |
| Customer | Precision parts injection molding company |
| Processing | Plastic molding |
| Mold standard | HASCO |
| Category | Injection Molds |
Typical applications for this kind of part:
Send the drawing and we will quote it using this project as a reference.
Our after-sales team supports mold maintenance and modifications remotely and can supply spare inserts. Contact customerservice@precisemoulds.com.
It uses hardened steels, hot runners, stronger alignment and optimised cooling, designed for long life and short cycles. A prototype mold uses softer materials and simpler construction for low cost.
Typically from several hundred thousand to over a million shots, depending on steel, resin and maintenance.
Yes. We recommend a set of wear spares, such as ejector pins and inserts, and provide drawings so you can order more later.
More injection molds engineered by our team.
Single-cavity DIN 1.2344 mold with a YUDO hot runner, lifters and slides for a 20% GF PA66 interior cabinet.
Long-life production mold for visible electronic parts with strict parting-line requirements.
Engineering detailsMulti-impression H13 mold for small consumer-electronic parts with tight cavity-to-cavity consistency.
Large single-cavity tooling for curved interior trim, machined on large-stroke CNC and double-head EDM.
Engineering detailsGet a quote
Share a 3D file, 2D drawing, sample photo or sketch. A mold engineer — not a sales robot — checks moldability before we quote tooling and part price.


