 Insert molding
 Overmolding
 Unscrewing molds
 Automotive
 Electronics
 Home appliance
 Industrial equipment
 Medical devices
 Machinery & automation


Mold
Molds
Multi-Cavity Mold for Precision Parts
Multi-impression H13 mold for small consumer-electronic parts with tight cavity-to-cavity consistency.
30% GF filled PA66AISI H132 cavities
Engineering details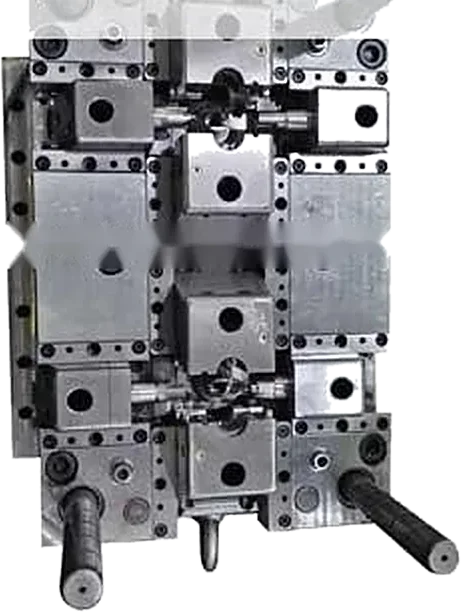 Click to zoom
Multi-cavity H13 unscrewing mold for externally threaded 30% glass-filled PA parts.
| Part material | 30% glass filled PA |
|---|---|
| Cavity / core steel | AISI H13 |
| Runner system | Cold runner |
| Cavities | Multi cavities |
| Processing | Plastic molding |
| Mold standard | HASCO |
A multi-cavity unscrewing mold has a more complex structure than a single-cavity one: several threaded cores must rotate together, driven by one gear train, while every cavity fills and cools identically. Designing and building such a mold needs an experienced engineering team and mold makers who have done it many times.
The parts in this mold have external threads, which often must be molded with an extremely fine parting line, or with no visible parting line at all, so the thread seals and looks clean. That rules out simple split cavities and calls for rotating thread rings or very precise slides.
We run the mold on our presses and check threads from every cavity with gauges, along with cycle time and the smooth running of the unscrewing mechanism.
| Part material | 30% glass filled PA |
|---|---|
| Tooling made in | China |
| Cavity / core steel | AISI H13 |
| Runner system | Cold runner |
| Cavities | Multi cavities |
| Customer | Auto injection molding company |
| Processing | Plastic molding |
| Mold standard | HASCO |
| Category | Injection Molds |
Typical applications for this kind of part:
Send the drawing and we will quote it using this project as a reference.
Our after-sales team supports mold maintenance and modifications remotely and can supply spare inserts. Contact customerservice@precisemoulds.com.
All threaded cores must rotate in sync through one drive, with identical cooling and filling in every cavity. Small errors in gear fitting or alignment show up as thread defects in some cavities.
Yes, by unscrewing the part out of a rotating thread ring instead of splitting the cavity. This gives a clean, continuous thread.
Commonly 2 to 16, depending on part size and press. We recommend the count after reviewing volume and thread geometry.
More injection molds engineered by our team.
Multi-impression H13 mold for small consumer-electronic parts with tight cavity-to-cavity consistency.
Single-cavity H13 unscrewing mold with hot runner for a POM threaded part, cylinder-driven rotation.
Large single-cavity tooling for curved interior trim, machined on large-stroke CNC and double-head EDM.
Engineering details1+1 family mold in H13 that molds two different ABS electronic parts in one shot.
Get a quote
Share a 3D file, 2D drawing, sample photo or sketch. A mold engineer — not a sales robot — checks moldability before we quote tooling and part price.