
 Insert molding
 Overmolding
 Unscrewing molds
 Automotive
 Electronics
 Home appliance
 Industrial equipment
 Medical devices
 Machinery & automation


Unscrewing
Unscrewing
Unscrewing Mold for Pipe Fitting Parts
Threaded Y-type pipe fitting in 30% GF PA66, two-cavity unscrewing mold with sealing-critical threads.
30% GF filled PA66AISI H132 cavities
Engineering details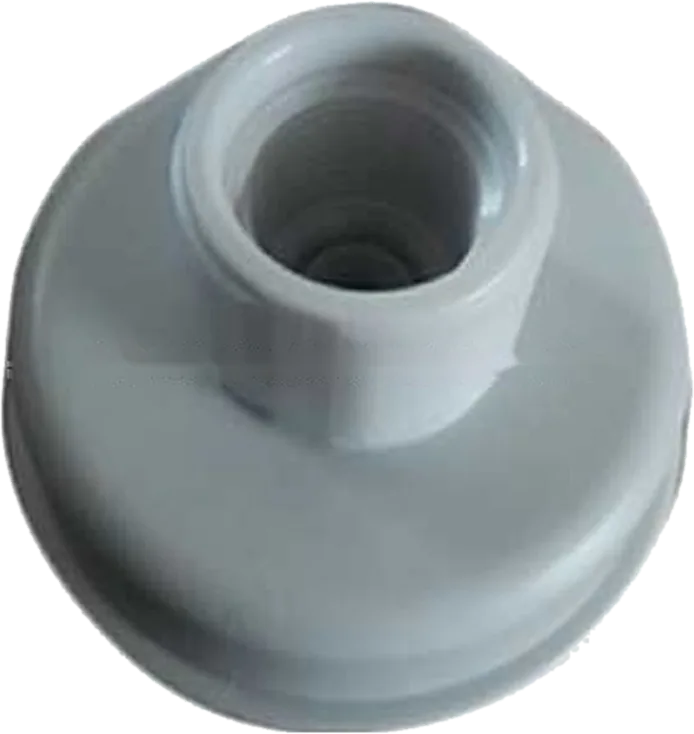 Click to zoom
Two-cavity DIN 1.2344 unscrewing mold producing threaded PA66 caps without stripping the thread.
| Part material | PA66 |
|---|---|
| Cavity / core steel | DIN 1.2344 |
| Runner system | Cold runner |
| Cavities | 2 cavities |
| Processing | Plastic molding |
| Mold standard | HASCO |
A threaded cap cannot simply be pushed off its core: a full, deep thread would be damaged or the part would deform. This PA66 cap is released by an unscrewing mold, in which the threaded core rotates out of the part before ejection. The result is a complete, accurate thread that seals properly on its mating part.
Unscrewing can be driven by a hydraulic cylinder with a rack, or by a hydraulic or electric motor. A cylinder drive gives an exact start and end of rotation and is easy to control, but it needs more space. A motor drive is compact but harder to stop at an exact position because of inertia. We choose the drive based on thread length, cavity count and the press the mold will run on.
Every unscrewing mold is run on our presses at T1 so the thread, sealing face and cycle are proven before shipment.
| Part material | PA66 |
|---|---|
| Tooling made in | China |
| Cavity / core steel | DIN 1.2344 |
| Runner system | Cold runner |
| Cavities | 2 cavities |
| Customer | Plastic molding company |
| Processing | Plastic molding |
| Mold standard | HASCO |
| Category | Unscrewing Parts |
Typical applications for this kind of part:
Send the drawing and we will quote it using this project as a reference.
Our after-sales team supports mold maintenance and modifications remotely and can supply spare inserts. Contact customerservice@precisemoulds.com.
When it has full internal or external threads that cannot be stripped or collapsed off the core without damage, especially in rigid or glass-filled materials and on sealing threads.
DIN 1.2344 (similar to H13) can be hardened for wear resistance and keeps its strength at molding temperatures, which suits rotating threaded cores that see friction every cycle.
Yes. Several cores can be driven by one gear train. We build multi-cavity unscrewing molds where volume justifies it.
More unscrewing parts engineered by our team.
Threaded Y-type pipe fitting in 30% GF PA66, two-cavity unscrewing mold with sealing-critical threads.
Multi-cavity H13 unscrewing mold for externally threaded 30% glass-filled PA parts.
Automotive pipe fitting with several threaded ports in 30% GF PA66, two-cavity unscrewing mold.
Threaded multi-port pipe connector in 30% GF PA66, two-cavity unscrewing tool.
Get a quote
Share a 3D file, 2D drawing, sample photo or sketch. A mold engineer — not a sales robot — checks moldability before we quote tooling and part price.


