
 Insert molding
 Overmolding
 Unscrewing molds
 Automotive
 Electronics
 Home appliance
 Industrial equipment
 Medical devices
 Machinery & automation


Unscrewing
Unscrewing
Unscrewing Mold for Threaded Cap Parts
Two-cavity DIN 1.2344 unscrewing mold producing threaded PA66 caps without stripping the thread.
PA66DIN 1.23442 cavities
Engineering details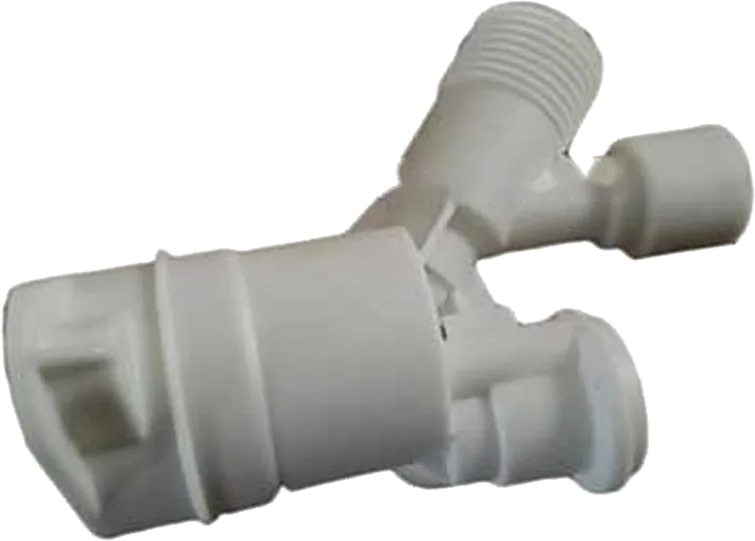 Click to zoom
Threaded Y-type pipe fitting in 30% GF PA66, two-cavity unscrewing mold with sealing-critical threads.
| Part material | 30% GF filled PA66 |
|---|---|
| Cavity / core steel | AISI H13 |
| Runner system | Cold runner |
| Cavities | 2 cavities |
| Processing | Plastic molding, injection molding |
| Mold standard | HASCO |
This Y-type pipe fitting has threaded connections that must seal against their mating pipes. Sealing is the key to a successful pipe-fitting mold: a thread with flash, a mismatch at the parting line or a deformed start will leak. We make these molds with unscrewing cores that rotate out of the threads instead of stripping them.
An unscrewing mold contains a mechanism inside the mold: threaded cores, gears or racks, bearings and a drive. In a fitting with several ports, cores may also need to pull in different directions. All of this has to fit around cooling and ejection without weakening the steel.
Our engineering team designs the action structure, and experienced toolmakers fit it under our quality system. Every unscrewing mold is proven on our presses: we check thread gauges, sealing faces and cycle time before shipment, so the mold you receive works as promised.
| Part material | 30% GF filled PA66 |
|---|---|
| Tooling made in | China |
| Cavity / core steel | AISI H13 |
| Runner system | Cold runner |
| Cavities | 2 cavities |
| Customer | Auto injection molding company |
| Processing | Plastic molding, injection molding |
| Mold standard | HASCO |
| Category | Unscrewing Parts |
Typical applications for this kind of part:
Send the drawing and we will quote it using this project as a reference.
Our after-sales team supports mold maintenance and modifications remotely and can supply spare inserts. Contact customerservice@precisemoulds.com.
Fittings carry fluid under pressure. Flash, mismatch or a deformed thread creates a leak path, so the thread and sealing surfaces must be molded perfectly every shot.
Yes, with side cores and unscrewing cores pulling in different directions. The mold is more complex, but you avoid assembling and sealing separate parts.
With thread gauges, visual inspection of the thread start and sealing face, and dimensional measurement of the critical diameters.
More unscrewing parts engineered by our team.
Two-cavity DIN 1.2344 unscrewing mold producing threaded PA66 caps without stripping the thread.
Multi-cavity H13 unscrewing mold for externally threaded 30% glass-filled PA parts.
Automotive pipe fitting with several threaded ports in 30% GF PA66, two-cavity unscrewing mold.
Threaded multi-port pipe connector in 30% GF PA66, two-cavity unscrewing tool.
Get a quote
Share a 3D file, 2D drawing, sample photo or sketch. A mold engineer — not a sales robot — checks moldability before we quote tooling and part price.


