 Insert molding
 Overmolding
 Unscrewing molds
 Automotive
 Electronics
 Home appliance
 Industrial equipment
 Medical devices
 Machinery & automation


Mold
Molds
Injection Mold for Single-Use Medical Devices
High-volume tooling for disposable medical plastic parts, designed for low cost per part.
Engineering details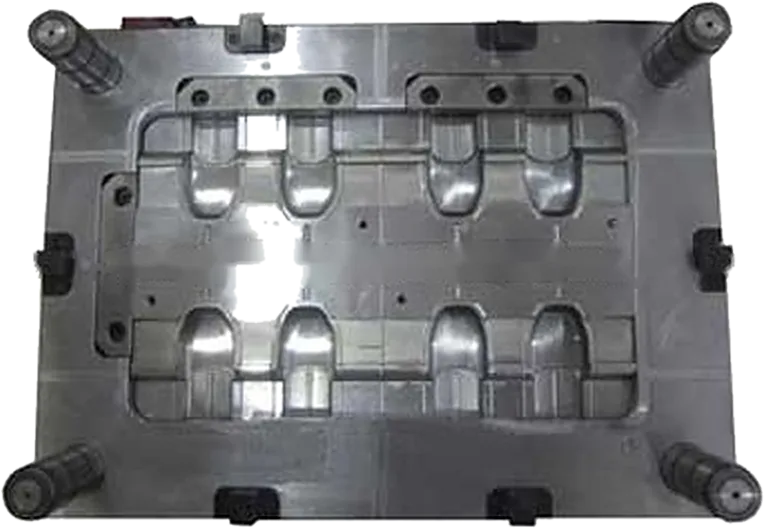 Click to zoom
Multi-impression H13 mold for small consumer-electronic parts with tight cavity-to-cavity consistency.
| Part material | 30% GF filled PA66 |
|---|---|
| Cavity / core steel | AISI H13 |
| Runner system | Cold runner |
| Cavities | 2 cavities |
| Processing | Plastic molding |
| Mold standard | HASCO |
A multi-cavity mold produces several identical parts in each shot. For small precision parts in consumer electronics, that is the only way to reach the volumes and part prices the market expects. But every cavity must produce the same part: if one cavity runs slightly bigger or fills later, the parts from that cavity fail inspection.
This mold uses AISI H13 cavities and a cold runner on a HASCO base, listed for 30% glass-filled PA66 parts.
Consumer electronics change every season, sometimes every few months. A mold maker with complete machining capacity in-house can keep the mold schedule under control. Our project management team follows every step of component machining, and every component is inspected before assembly, so the mold reaches T1 on time.
| Part material | 30% GF filled PA66 |
|---|---|
| Tooling made in | China |
| Cavity / core steel | AISI H13 |
| Runner system | Cold runner |
| Cavities | 2 cavities |
| Customer | Auto injection molding company |
| Processing | Plastic molding |
| Mold standard | HASCO |
| Category | Injection Molds |
Typical applications for this kind of part:
Send the drawing and we will quote it using this project as a reference.
Our after-sales team supports mold maintenance and modifications remotely and can supply spare inserts. Contact customerservice@precisemoulds.com.
It depends on part size, tolerance and press size. Small parts often run in 4, 8 or 16 cavities; very tight tolerances may favour fewer cavities for better control.
Cavities are machined from the same programs, measured on CMM, and the runner is balanced. At T1 we measure parts from every cavity and correct any differences.
For high volumes it often is: it removes runner scrap and balances filling more easily. For moderate volumes a well-balanced cold runner is more economical.
More injection molds engineered by our team.
High-volume tooling for disposable medical plastic parts, designed for low cost per part.
Engineering detailsSingle-cavity H13 unscrewing mold with hot runner for a POM threaded part, cylinder-driven rotation.
Multi-cavity H13 unscrewing mold for externally threaded 30% glass-filled PA parts.
Large single-cavity tooling for curved interior trim, machined on large-stroke CNC and double-head EDM.
Engineering detailsGet a quote
Share a 3D file, 2D drawing, sample photo or sketch. A mold engineer — not a sales robot — checks moldability before we quote tooling and part price.